Quality Assurance
Our commitment to consistent, reliable product quality
Quality at Every Stage
Krishna Ink is committed to delivering printing inks and chemicals that consistently meet customer specifications and application requirements. Quality management is integral to our manufacturing process, from raw material selection through to finished product despatch.
In the industrial printing sector, even minor variations in pigment grind, solvent volatility, or polymer tack can trigger significant downtime, color drift, and substrate adhesion failures. That is why our quality framework is built around repeatability, continuous in-line verification, and strict laboratory validation.
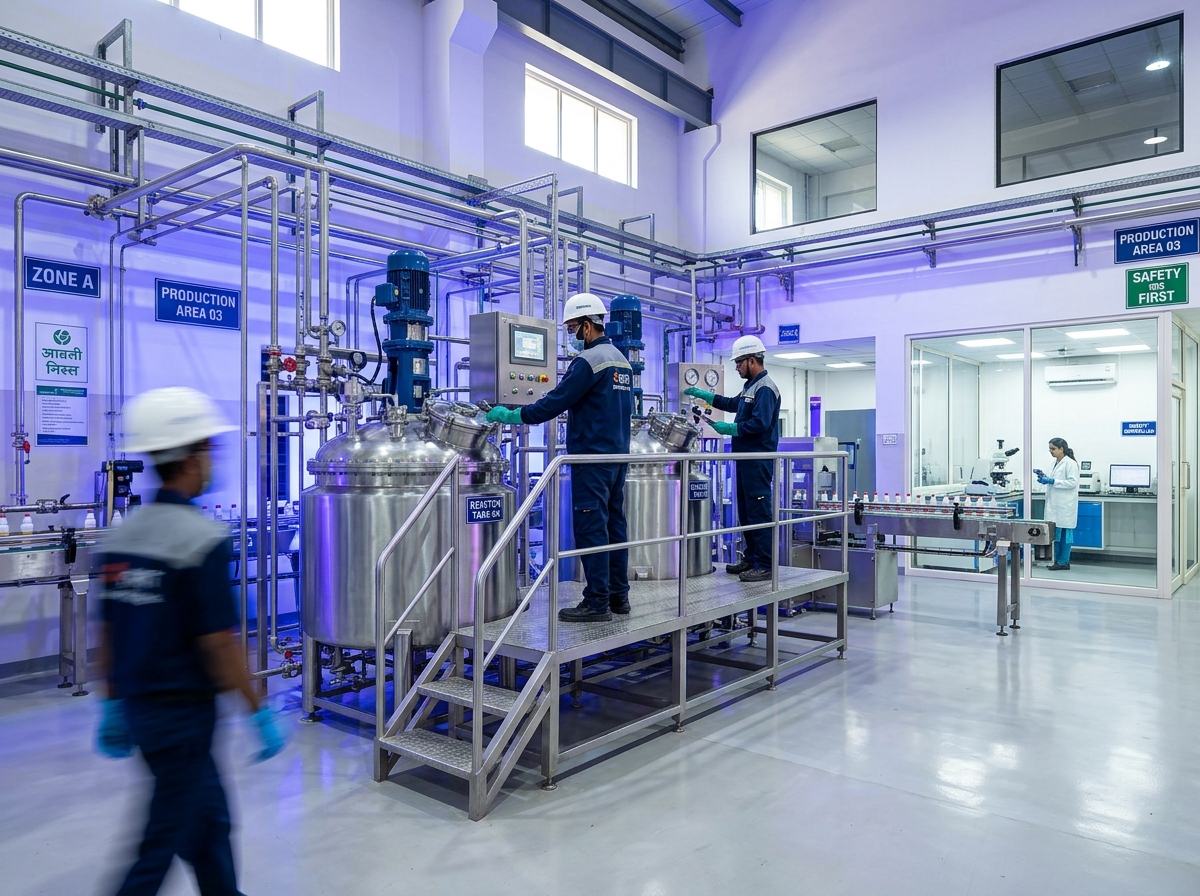
Every production batch is identified with a unique lot number, enabling end-to-end traceability back to initial raw material certificates of analysis. Our quality control technicians perform standardized test protocols for dispersion, viscosity, drying rates, and color values before any container is approved for sealing.
Our 5-Stage Manufacturing Process
A systematic, documented workflow ensures that every litre of ink and chemical produced in our plant satisfies strict industrial criteria before reaching our clients' pressrooms.
Raw Material Selection
Sourcing and rigorous evaluation of input pigments, resins, technical solvents, and performance additives strictly from qualified, reliable chemical manufacturers with certified purity specs.
Incoming Material Inspection
Comprehensive quality verification of incoming raw materials before production release. Testing includes moisture titration, density analysis, solvent purity assay, and baseline color strength.
In-Process Quality Monitoring
Controlled production with regular in-process checks during triple-roll dispersion, bead milling, and high-shear blending. Particle fineness is checked with Hegman grind gauges.
Finished Product Testing
Exhaustive testing of colour against master digital standards, rotational viscosity, tack, drying speed, and substrate adhesion properties before granting final quality sign-off.
Packaging and Despatch
Correct packaging in industrial-grade, vapor-tight containers, precision labelling with batch barcodes, safety notices, and secure, tamper-evident despatch to customer locations.
Core Quality Standards
We maintain strict operational tolerances across three critical performance pillars that define runnability and visual excellence on the printing floor.
Colour Consistency
Batch-to-batch colour matching to maintain consistency across orders. Every batch is evaluated against retained standard master specimens using spectrophotometric Delta-E color evaluation under standardized D50/D65 illuminants.
- Strict Delta-E tolerance limits
- Archived retention samples for every batch
- Digital spectral reflectance verification
Viscosity Control
Formulated to application-appropriate viscosity ranges for printability. We verify shear-dependent flow characteristics utilizing calibrated rotational viscometers and standardized efflux flow cups across temperature-regulated environments.
- Rotational viscometer rheology profiles
- Temperature-compensated flow testing
- Thixotropic index optimization for screens and rollers
Application Testing
Representative application testing where applicable before release. Our in-house proofing studio prints trial drawdowns onto production-grade films, papers, and fabrics to confirm adhesion, cure time, rub fastness, and surface finish.
- Cross-hatch tape adhesion checks (ASTM D3359)
- Sutherland-style rub and scuff evaluations
- Wash-fastness and crocking testing for textiles
Quality Documentation & Certification
Product certifications, Certificates of Analysis (COA), and formal quality documentation are available upon enquiry for relevant product lines. Please contact our technical compliance team with your specific lot or purchase order number.
Responsible Manufacturing
Krishna Ink acknowledges the importance of responsible manufacturing and supply. We work to source materials responsibly, handle chemicals safely, and provide customers with appropriate safety information for our products. Specific sustainability data and formal reports are in development.
Our operations prioritize solvent recovery, closed-loop wash stations, and the systematic elimination of prohibited substances from our raw material matrix. We are dedicated to continuous operational improvements that reduce waste while preserving the unmatched technical performance our industrial partners depend upon.